


Views: 0 Author: Site Editor Publish Time: 2026-11-13 Origin: Site


Ordering ceramic decorations in bulk is a massive financial commitment for retailers, wholesalers, and event planners. Ceramics offer high profit margins and timeless aesthetic appeal. Yet, they are fundamentally fragile. Manufacturing inconsistencies happen daily on the factory floor. Finding the right design is merely the first step. Ensuring flawless execution is where the real procurement battle lies. A rigorous inspection process before finalizing a mass order prevents dead stock. It protects your brand reputation. This technical guide breaks down exactly what B2B buyers must scrutinize on the production line, moving from raw clay chemistry to final packaging standards.
Request Pre-Production Samples: Always inspect a physical master sample to verify shape, volumetric shrinkage, and glaze chemistry before authorizing mass runs.
Check Structural Integrity: Intricate designs require strict wall thickness tolerances. Ensure negative spaces have smooth, deburred edges.
Evaluate Glaze and Finish: Look for chemical defects like pinholes, crazing, or crawling that ruin the specular reflection of premium decorations.
Verify Uniformity: Bulk orders demand strict consistency in dimensions and mass to avoid downstream packaging bottlenecks.
Prioritize Safe Packaging: Demand empirical drop-test reports and custom die-cut foam to guarantee transit survivability.
Market data reveals a sharp pivot in how global buyers source home decor. The outdated model of sorting out defective units after delivery is no longer viable. Volatile ocean freight rates make shipping unmarketable goods a severe financial liability. Today, leading importers demand proactive quality control directly on the production line. There is a growing emphasis on zero-waste manufacturing and sustainable procurement. Factories face tighter tolerances for complex geometries. Buyers expect premium, flawless finishes without accepting the traditional defect rates. This industry-wide shift forces brands to implement rigorous pre-production evaluations rather than relying on post-shipment sorting.
When purchasing commercial quantities, a minor mold flaw quickly multiplies into thousands of unsellable units. Unlike stamped metals, ceramics are vitrified mineral products. They undergo extreme physical and chemical transformations in the kiln. Small oversights in raw slip preparation manifest as structural weaknesses across entire batches.
A standard shipping container holds tens of thousands of decorative items. If an unchecked casting defect compromises a run, the financial liability extends far beyond the initial invoice. Importers face sunk ocean freight fees, wasted customs duties, and massive domestic disposal costs. Establishing a disciplined inspection procedure eliminates unsellable stock before units clear the factory loading dock.
Furthermore, product finish directly impacts perceived brand equity. Retail customers expect uniform coloring, smooth touchpoints, and stable bases. Rough edges or structural instability lead to high return rates and damaging reviews. Consistent incoming quality protects your shelf presence.
Manufacturing facilities operate according to tolerances defined in your contract. Without explicit quality metrics, factories default to their internal benchmarks. These rarely align with premium retail requirements. By defining an Acceptable Quality Limit, buyers give factory floor managers precise targets for sorting and quality grading.
A beautiful design means nothing if the underlying clay body is weak. The durability and tactile feel of decorative ceramics start with the raw slip formulation. Discrepancies in kiln soaking times undermine the entire matrix.
Wholesale buyers must evaluate if the clay matches the functional demands. Earthenware yields a porous core that chips easily. In contrast, stoneware offers high mechanical strength ideal for everyday handling. Porcelain provides exceptional hardness. Ensure the supplier’s firing temperature matches the agreed specifications. Under-firing leaves the core soft and brittle.
Pick up the sample. A well-fired ceramic piece exhibits a balanced hand-feel. Measure the mass against your engineering tech pack using a precision digital scale. Unexpected lightness points to uneven slip casting, excess water in the slurry, or hidden internal voids.
Internal micro-fractures from thermal shock are invisible to the naked eye. The acoustic ring test is a fast, non-destructive diagnostic tool. Suspend the item lightly and tap the body with a plastic rod. A clear, sustained ring confirms a dense matrix. A dull thud signals severe sub-surface porosity. Flag it as a structural reject immediately.
Architectural and pierced home accessories represent high-margin retail categories. However, their complex geometry makes them highly vulnerable on the factory floor. Negative spaces and delicate corners concentrate mechanical stress during drying and firing.
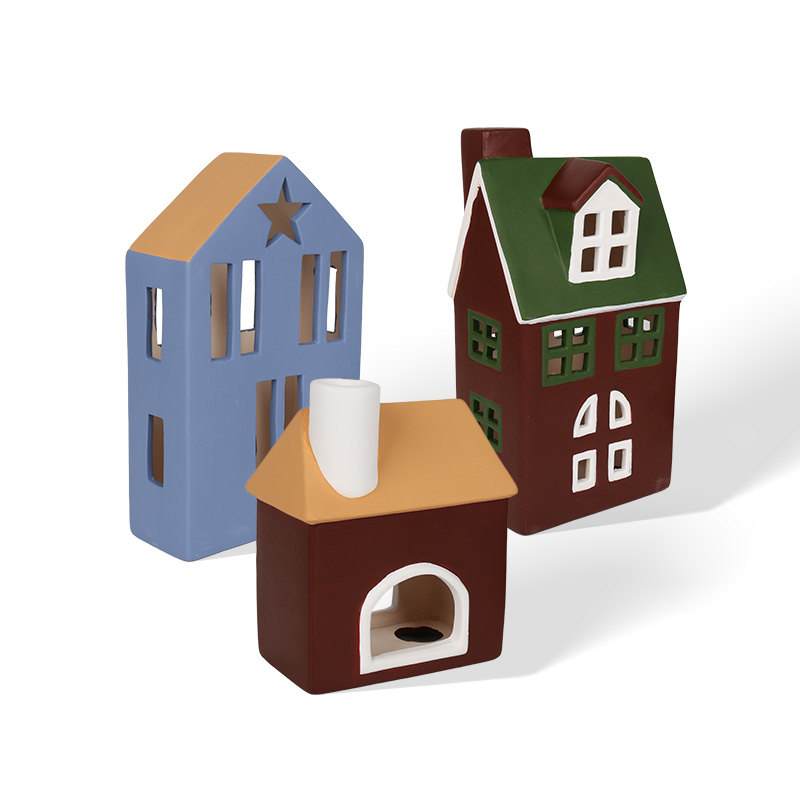
Pierced designs require manual greenware trimming prior to the bisque fire. When inspecting Hollow Cutout Ceramic House Ornaments, look closely at the cutout perimeters. The inner walls must be clean, thoroughly deburred, and sponge-finished. Watch for feathering. This thin clay flash breaks off easily during shipping, leaving raw, unglazed patches.
Symmetry is critical for architectural forms. When reviewing Hollow Window Frame Ceramic House Ornaments, check the internal corners. Surface tension causes thick glazes to bridge small gaps, rounding off sharp details. Differential shrinkage pulls delicate mullions out of square, causing visible warping.
Scaled-down decor demands strict wall thickness control. Items like Hollow Cutout Mini Ceramic House Ornaments are highly susceptible to transit impact damage. Anything below a 2.5 mm cross-section is a major risk. Use vernier calipers to verify uniform thickness throughout the casting profile.
Parameter | Standard Tolerance | Critical Defect Trigger | Inspection Method |
|---|---|---|---|
Wall Thickness | 3.5mm - 5.0mm | Below 2.5mm (High fracture risk) | Vernier Caliper across multiple points |
Base Flatness | Gap < 0.5mm | Wobbles under applied finger pressure | Feeler Gauge on granite surface plate |
Firing Temperature | 1050°C - 1220°C (Stoneware/Dolomite) | High water absorption rate | Acoustic ring test / Moisture meter |
Dimensional Variance | ± 3% from tech pack | Fails to fit internal blister pack | Calibrated Go/No-Go Gauge |
Glazes are vitreous coatings melted in place to provide color and protection. Bad chemistry disrupts the visual appeal and exposes the porous clay body to moisture.
Systematic inspection requires a well-lit booth with 5000K daylight illumination. Rotate the piece slowly. Pinholes interrupt the specular reflection. Crazing shows a network of fine hairline fractures indicating residual tensile stress. Crawling leaves patches of exposed clay. None of these belong on premium retail items.
Kiln atmospheres fluctuate based on burner performance and airflow. This creates shade variations across production runs. Establish a physical color tolerance range using master plaques. Use a spectrophotometer to confirm units stay within an agreed Delta E variance threshold. Mismatched tones kill retail set sales.
The tactile quality must match the approved specifications. Matte glazes must feel silky, not chalky or abrasive. Reactive glazes must fall within defined visual boundaries for crystal size and phase separation. The surface must evoke the premium quality your brand promises.
Clay shrinks up to 15% as water is driven out during firing. Controlling this volumetric contraction across mass production requires precise mold management.
Significant dimensional variations cause immediate supply chain bottlenecks. If an ornament is just three millimeters too tall, it crushes the retail carton. Confirm outer boundary dimensions with calibrated gauges, keeping thresholds tight.
A wobbly base is unacceptable for tabletop decor. Position the piece on a ground-glass surface plate. Apply alternating vertical pressure to the rim. Gaps exceeding 0.5 mm require mechanical bottom grinding. Ensure unglazed footrings are polished smooth to protect household furniture.
Slip-casting relies on plaster molds that deteriorate over time. As a mold absorbs water through repeated cycles, sharp internal details soften. Compare early-production pieces against late-production units. If architectural lines lose their sharpness, the factory must retire the worn molds and pour fresh master cases.
Never skip the pre-production sample phase. The physical sample serves as your definitive contract. It establishes the exact standard the mass run must meet. Relying solely on digital renderings is a high-risk strategy. B2B buyers must conduct a rigorous evaluation before transferring the production deposit.
Start by confirming physical dimensions against the original tech pack. Because clay warps, use digital calipers to measure height, width, and depth. This precision is vital for complex designs like Hollow Window Ceramic House Ornaments, where a minor deviation distorts visual symmetry.
Inspect the sample under standardized D65 lighting to evaluate true color fidelity and opacity. Ensure there are no unintentional color variations caused by uneven kiln oxidation.
Brand visibility is paramount. Whether your logo is applied via water-slide decals or bottom stamping, it must be durable. Perform an adhesion test by applying transparent tape firmly over the logo and pulling it off quickly. If the ink flakes, the curing temperature was too low.
Many modern decorations incorporate secondary materials. If your product includes wooden bases, metal handles, or electronic components, test the integration. Ensure LED lights fit smoothly into base cavities and heat dissipation is adequate.
Perfectly crafted ceramics are worthless if they arrive shattered. Packaging inspection is a non-negotiable step. Standard factory packaging frequently leads to high defect rates upon delivery.
Inner packaging is the primary defense against transit vibration. Bubble wrap alone fails in bulk shipping. Inspect the packaging to ensure the factory uses custom die-cut Polyethylene foam that matches the exact contours of the piece. Delicate extremities must be protected from crushing forces.
Demand standardized empirical testing. Require an ISTA 1A drop test report. This protocol drops the fully packed master carton onto a hard surface across corners, edges, and flat faces. If a single piece chips, the packaging design fails.
The master carton protects your inventory during palletization. Verify the factory uses high-quality, double-wall corrugated cardboard with a high Edge Crush Test rating. Cartons must be sealed with reinforced tape and marked with clear fragility warnings.
Ensuring your manufacturing partner meets compliance standards mitigates legal risk. Certifications provide third-party validation of material safety and quality control systems.
Heavy metals like lead and cadmium were historically used in vibrant glazes. Buyers importing into strictly regulated markets must ensure products comply with laws like California Proposition 65. Demand recent laboratory test reports confirming glazes are free of leachable toxins.
Modern consumers demand ethical practices. Request documentation of social compliance audits, such as BSCI or Sedex SMETA. These evaluate fair wages, occupational health, and silica dust exposure control. Well-managed factories consistently produce higher quality goods.
Procuring ceramic decorations in commercial volumes requires a highly proactive approach to quality control. By executing a strict inspection checklist covering structural tolerances, glaze chemistry, and transit packaging, buyers secure their inventory investments. Do not let easily preventable factory errors erode your profit margins. Always insist on physical master samples, define strict numerical AQL standards, and demand drop-tested packaging. For B2B buyers seeking premium, rigorously inspected designs, exploring the extensive, quality-assured catalog at art-word.com provides a reliable pathway to scaling your home decor product lines.
In commercial ceramics manufacturing, absolute perfection across thousands of units is practically impossible due to the organic nature of clay. A standard Acceptable Quality Limit is typically set at 2.5% for major defects such as deep cracks or large chips, and 4.0% for minor defects like microscopic pinholes. You must negotiate and document this standard directly in your purchase agreement.
Protecting hollow elements requires a two-step approach. First, inspect the wall thickness around the cutouts using digital calipers to ensure the clay is robust enough to withstand handling. Second, insist on custom-molded inner packaging, such as die-cut PE foam, designed to fill the internal voids and support the hollow structures from the inside out.
Kiln firing naturally causes slight color shifts due to temperature gradients. Establish a formal tolerance range measured in Delta E values during the sampling phase. If the final bulk order falls outside this agreed-upon range, you can request a financial discount, demand a remake of the defective batch, or reject the shipment entirely before paying the balance.
The classification depends on the product's positioning. A few pinholes may be acceptable in rustic style ceramics where texture adds character. However, for premium or high-gloss decorations, pinholes are strictly considered a major defect. They disrupt the visual appeal and can trap dirt over time.
Yes, hiring a third-party inspection agency is highly recommended, especially for new manufacturing facilities. An independent agency performs a Pre-Shipment Inspection at the factory to systematically check product dimensions, glaze quality, structural integrity, and conduct drop tests before container loading.
Inline inspection occurs during active production, catching raw slip formulation or bisque firing errors early on the factory floor. Pre-shipment inspection happens after goods are fully manufactured and packed, focusing on final glaze quality, packaging integrity, and overall AQL compliance before the container is sealed.
Durability testing involves multiple phases. Acoustic ring tests are performed on the line to detect internal micro-fractures invisible to the eye. Additionally, ISTA drop testing on the master cartons ensures the product and packaging combination can survive severe transit impacts. Thermal shock testing is also applied to items meant to hold candles or endure temperature swings.


